Unexpected equipment failures can bring production to a halt, even when machinery received maintenance a few weeks earlier. A seized conveyor bearing can stop an entire production line, delay orders, and increase repair costs. Research published by the National Institute of Standards and Technology (NIST) found that manufacturers relying more heavily on predictive maintenance experienced 18.5% less unplanned downtime and 87.3% fewer defects than manufacturers relying more heavily on preventive maintenance.
These findings highlight how maintenance strategies can influence operational performance and equipment reliability. So if maintenance decisions can affect equipment lifespan, repair expenses, and production efficiency, which approach makes the most sense for your operation?
What is Preventive Maintenance?
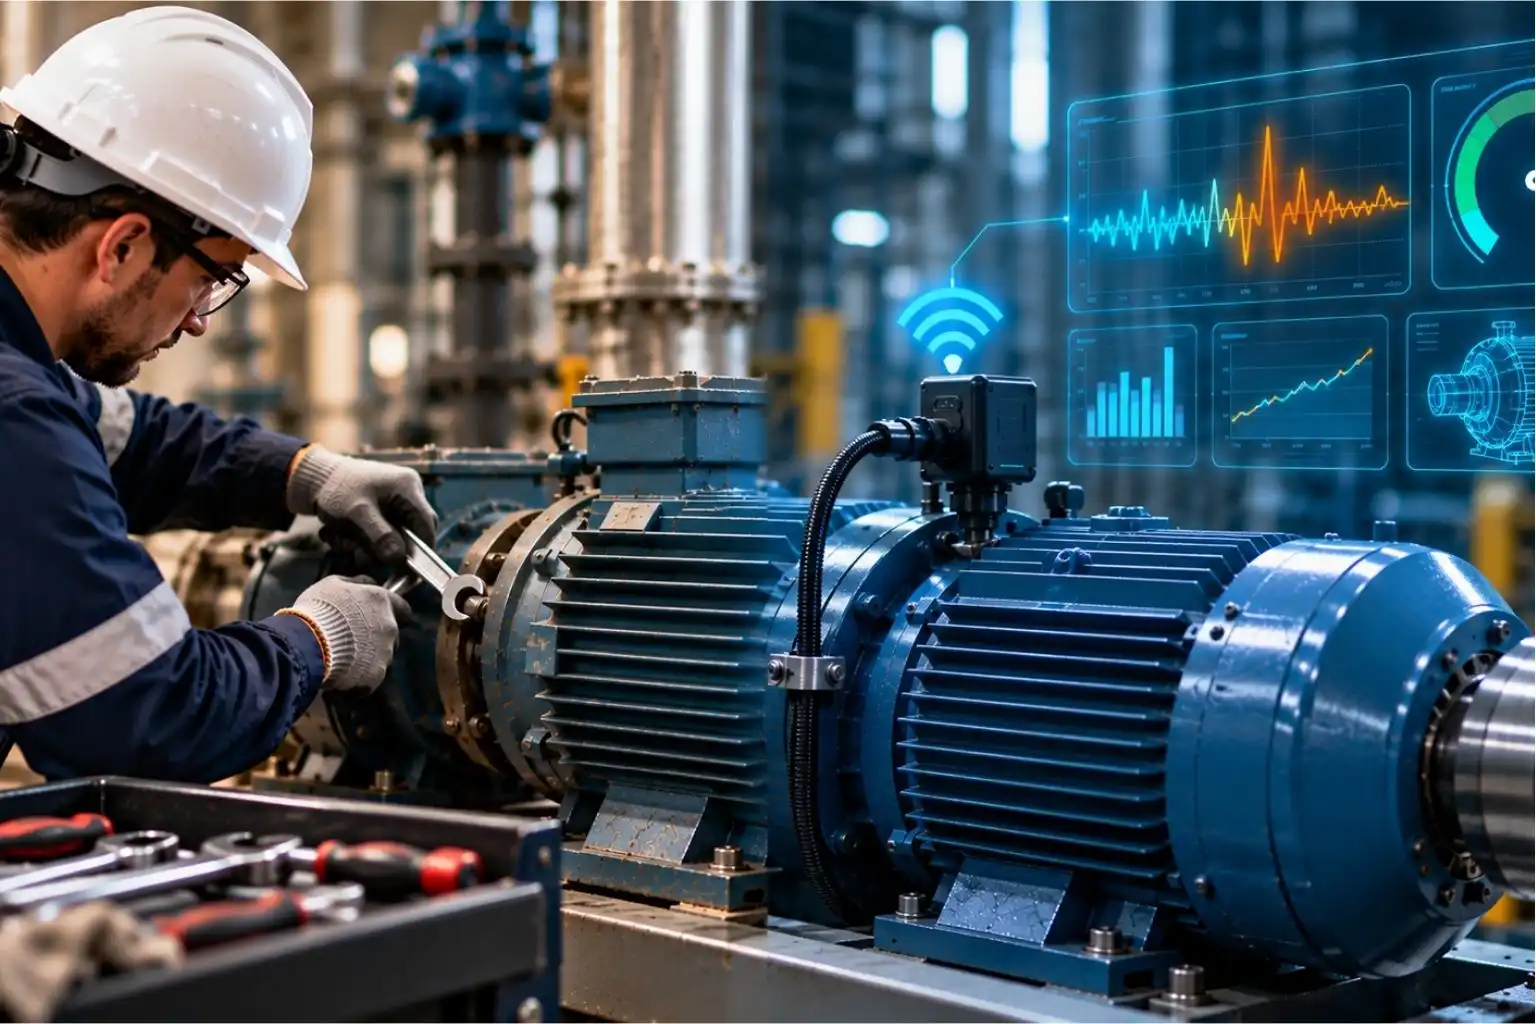
This approach works to a timetable. Preventative maintenance relies on planned tasks happening at fixed time or usage intervals, regardless of how the equipment looks on the day. The schedule usually starts with manufacturer recommendations and gets refined using your own service history, because preventive maintenance relies on that guidance and historical service history. Typical preventive maintenance tasks include:
- Lubricating and greasing conveyor bearings and other moving parts on a set schedule, since proper lubrication and alignment can extend asset lifespan
- Changing filters, belts and seals before they reach the end of their working life
- Carrying out routine inspections and guard checks at agreed intervals
It is simple to set up, runs with general technicians and starts paying off straight away. Its weak spot is timing, since a calendar has no way of knowing how hard a machine has actually worked, so parts can be replaced early, fail between visits, or create unnecessary tasks when components are changed too soon.
What is Predictive Maintenance?
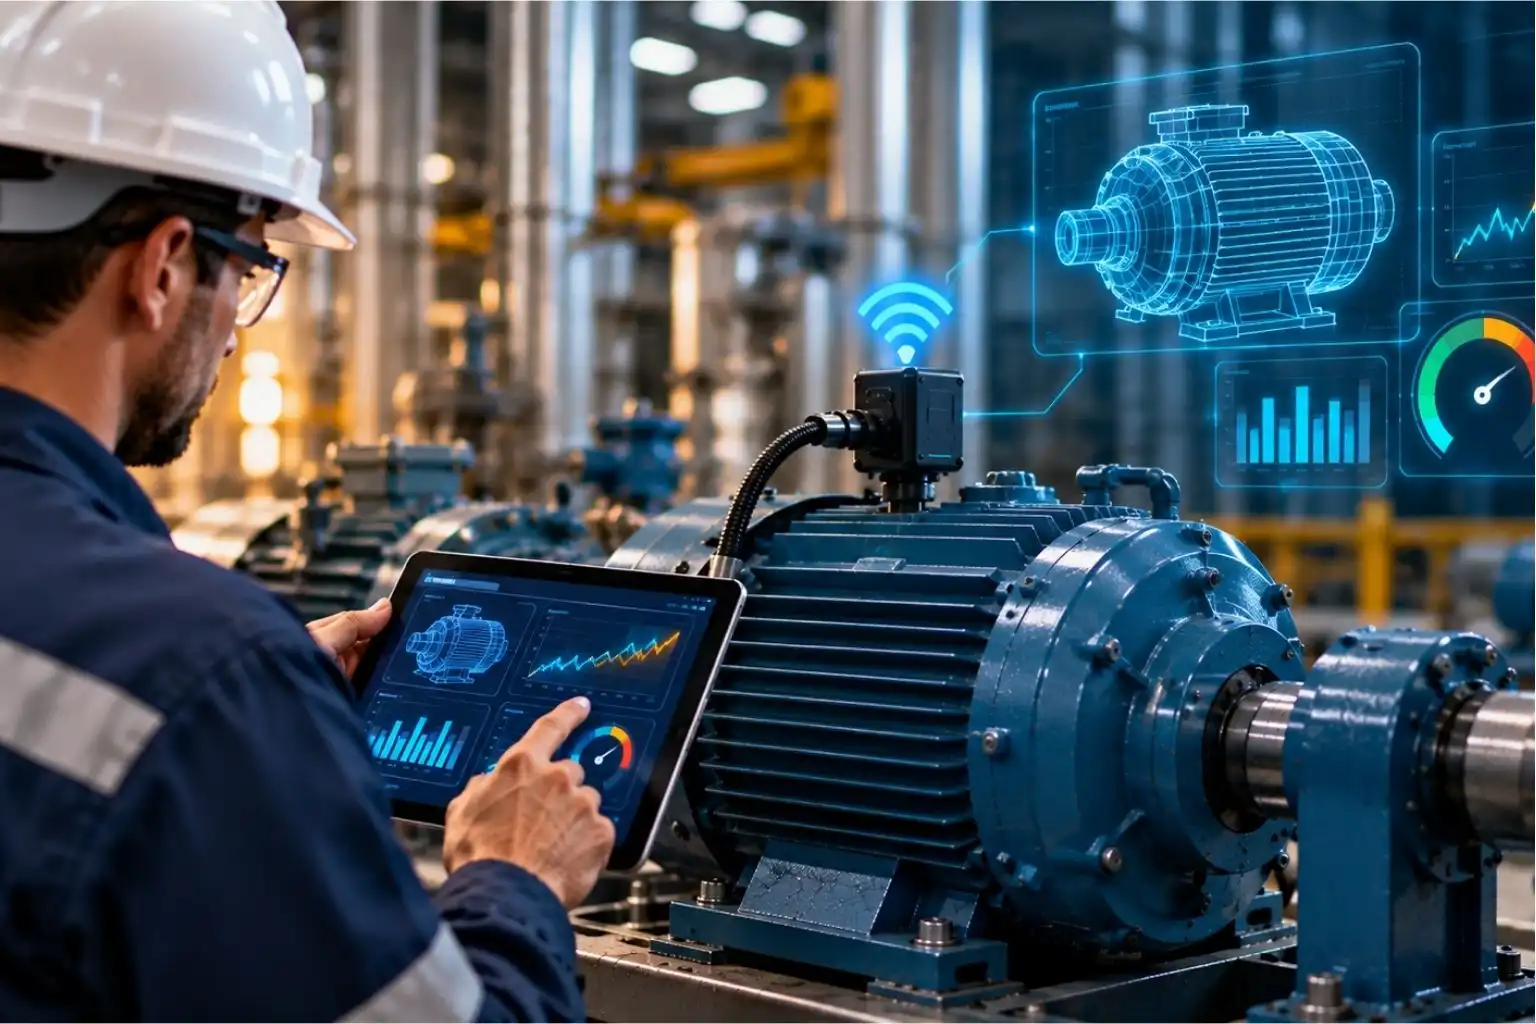
Here, the actual condition of an asset decides when work happens. It is a proactive approach that uses equipment data to anticipate equipment failures. Sensors and analytics track sensor data and other equipment data over time, spot trends and estimate when a failure is likely, giving a clearer view of asset health so engineers step in only when needed. Common monitoring methods include:
- Vibration analysis on rotating equipment to spot early warning signs such as bearing wear and misalignment weeks before a failure, supporting early fault detection and helping correct alignment and lubrication issues that extend asset life
- Temperature and infrared checks on motors, gearboxes and electrical connections
- Oil analysis, ultrasound and motor current readings to flag hidden deterioration
It asks more of a site than scheduled servicing. Predictive maintenance work depends on data analysis of operational data, often using machine learning within predictive maintenance systems and other predictive maintenance technologies. Sensors, software and someone skilled at interpreting the data all need to be in place, and the system needs several months of history before its forecasts become reliable. Until then, false alarms and data gaps can crop up. Maintenance teams also need clear maintenance workflows for acting on alerts.
What are the Trade-Offs Between Each Approach?
Here’s how scheduled and condition based maintenance servicing compare across trigger, cost, downtime, skills, time to value and the main risks involved:
| Factor | Preventive | Predictive |
|---|---|---|
| Trigger | Calendar or run-hour interval on a fixed schedule, set by maintenance schedules | Real-time condition data and trends used to schedule maintenance |
| Upfront cost | Low: schedules, checklists, basic software | High: sensors, software, analytics skills |
| Ongoing cost | Can rise through over-maintenance | Lower labour and parts spend once mature. Predictive maintenance reduces maintenance costs by avoiding emergency repairs and costly repairs |
| Downtime | Planned, often more frequent | Less overall, with teams able to schedule repairs to actual wear |
| Skills needed | General technicians | Reliability or data specialists |
| Time to value | Immediate | Several months |
| Main risk | Failures between intervals | Cost, false alarms, data gaps |
Some faults keep returning no matter which method you use, while reactive maintenance still has a place as a run-to-failure option for low-value assets. Where the same wear point appears in report after report, a redesign through our mechanical engineering team, such as a reworked drive, improved bearing housings or new guarding, can remove the failure altogether.
Where a machine is past the point a redesign can fix, the answer is often an upgrade. If it needs constant repairs, can’t keep up with output targets or relies on parts that are hard to source, maintenance alone won’t close the gap. For help deciding when to modernise or replace an asset, our guide to the signs your manufacturing equipment needs upgrading covers the warning signs to look out for.
How Do You Pick the Right Approach for Your Site?
Picking between the two is less about which method is better in theory and more about matching each one to the right equipment. Work through these steps asset by asset:
- Rank your equipment by criticality. Sort every machine into three tiers: critical assets, important machines with backups or known wear patterns, and low-value items you can safely run to failure.
- Put a price on an hour of downtime. Add up lost output, idle labour, wasted product and late delivery penalties. A filling line that loses thousands of pounds an hour justifies far more monitoring than a spare extraction fan.
- Look at how each asset fails. Your maintenance requirements matter here: predictable wear on belts, filters and seals often suits preventive maintenance, while monitorable failure modes on motors, bearings and gearboxes may justify predictive monitoring on high-priority equipment.
- Audit your existing schedule. Check how many planned jobs were completed on time last quarter. A preventive maintenance schedule within your wider maintenance program that slips by weeks needs fixing before any sensor goes in.
- Check your budget and skills. Predictive maintenance offers the most value where real time sensor data can be captured and used to guide maintenance resources. If that capability isn’t in-house, external industrial maintenance services can cover the inspection and repair side while you build it.
- Start small and expand. Fit monitoring to your top-tier assets first, keep fixed schedules everywhere else, and review the results after six to twelve months to build a small predictive maintenance program pilot before wider rollout. Done well, that helps keep operations running smoothly and cuts unplanned outages.
Monitoring often uncovers electrical faults such as overheating motors, loose wiring or tired control panels. Our electrical support handles the repair and upgrade work that follows, from fault-finding on electrical systems to replacing ageing controls, helping restore safe performance and lower energy consumption so your production line runs efficiently again.
Keep Every Shift Running Smoothly
Before spending a penny on sensors, pull last quarter’s maintenance records for the three machines that would stop production fastest and cause unexpected breakdowns. If planned jobs on those assets slipped or were skipped, tighten the schedule first. If the schedule ran on time and those machines still broke down, add condition monitoring to exactly those three assets and nothing else until the results come in. Focusing on the most critical assets is a practical way of reducing equipment failures and equipment downtime without creating extra maintenance tasks or unnecessary service elsewhere.
Singleton Engineering Solutions has supported manufacturers and food producers from its Burnley, Lancashire base since 2015, with engineers working on site right across the UK. Our maintenance and inspection preventive maintenance programs cover scheduled checks, servicing equipment and condition reports, focused on the equipment you can least afford to lose for asset uptime and cost savings. If you’re weighing up industrial maintenance services for your site, call 01282 423198, email office@singletonengineering.co.uk.
FAQs About Preventive and Predictive Maintenance
How quickly can you send an engineer to a production line breakdown?
How fast our engineers arrive depends on your location, the type of fault and availability at the time, with sites closer to our Burnley base reached sooner. To help us move quickly during a production line breakdown, have the machine details, a clear description of the fault and any recent service history ready when you call.
Photos or error codes help us bring the right parts and tools on the first visit. Once on site, our engineers focus on making the equipment safe and getting your line restarted, then recommend any follow-up repairs to stop the same fault returning. For confirmed attendance times at your site, speak to us directly.
Can you make replacement parts for older or obsolete machinery?
When the original manufacturer no longer supplies a part, we can often produce a suitable replacement in-house. Using the worn or broken component, along with any drawings you have, we measure and recreate it through our fabrication and manufacturing services, with precise steel components cut on our CNC profiling equipment.
This approach works well for brackets, guards, conveyor frames, mounting plates and other steel parts on older machinery. Making replacement parts for obsolete machinery can also extend the life of equipment that still performs well, avoiding the cost and disruption of a full replacement. Send us details, measurements or photos of the part, and our team will confirm what’s achievable.
Can you assess our site and tell us which machines need condition monitoring?
Yes, our engineers can visit your site, review your equipment and help you decide where condition monitoring will make the biggest difference. We look at how critical each machine is to production, how it tends to fail and what an hour of downtime on that asset would cost you, using maintenance history alongside service records and breakdown history. From there, we recommend which assets would benefit from closer monitoring and where a blend of preventive maintenance tasks and predictive monitoring is the better fit for each piece of equipment.
From there, we recommend which assets would benefit from closer monitoring and which are better kept on planned maintenance schedules. Teams should also create clear processes for responding to maintenance alerts and turning findings into planned work. You receive clear condition reports, so you can focus your budget on the equipment you can least afford to lose rather than monitoring everything at once, with the aim of reducing overall maintenance costs. To arrange a site assessment, contact us with a list of your key machines and any recent maintenance records.
Do you offer planned maintenance contracts for factory and production equipment?
We do. Our planned maintenance programmes are built around your equipment, production schedule and the machines that matter most to your output. Each programme can include scheduled servicing, routine inspections, guard checks and condition reports, with visit intervals set according to each machine’s workload, age and manufacturer guidance rather than a one-size-fits-all calendar.
Regular visits from the same team also mean our engineers get to know your equipment, which makes it easier to spot developing faults early and plan repairs around your production rather than reacting to breakdowns. If recurring problems show up in the reports, we can recommend longer-term fixes through our mechanical engineering or fabrication services. Get in touch with details of your site and equipment, and we’ll put together a maintenance programme that suits how your operation runs.